VanTsteri's company account describes an infection incident at an anonymous SPF research animal facility covering approximately 2,000 m². The investigation considered animal housing, support spaces and the ventilation system.
Investigation and response
The source reports that an external identification service identified ticks found during the investigation. The response combined vector-control measures, changes to filtration and environmental decontamination using vaporized hydrogen peroxide. Chemical and spore biological indicators were used to evaluate the treatment.
Company-reported outcome
The account describes three days of treatment followed by a one-week closure before restart. It reports that subsequent observation found no further tick-associated transmission. The observation period and underlying test records are not specified.
Scope of this account
This is an anonymous company-reported project, distinct from the pre-operational 450 m² SPF facility case. It does not establish a measured log reduction, permanent protection or an animal-health guarantee.
Coordinated treatment across four production lines and the production environment.
A large site with complex production systems
A large pet food manufacturer identified Salmonella contamination and engaged VanTsteri to investigate and address it. The plant operated four production lines, including lines with daily capacities of 10 tonnes or 8 tonnes. The project involved an actual treatment area of 50,000 m², as confirmed by VanTsteri’s project representative. Its scale and the complexity of the production systems created challenges for the on-site work.
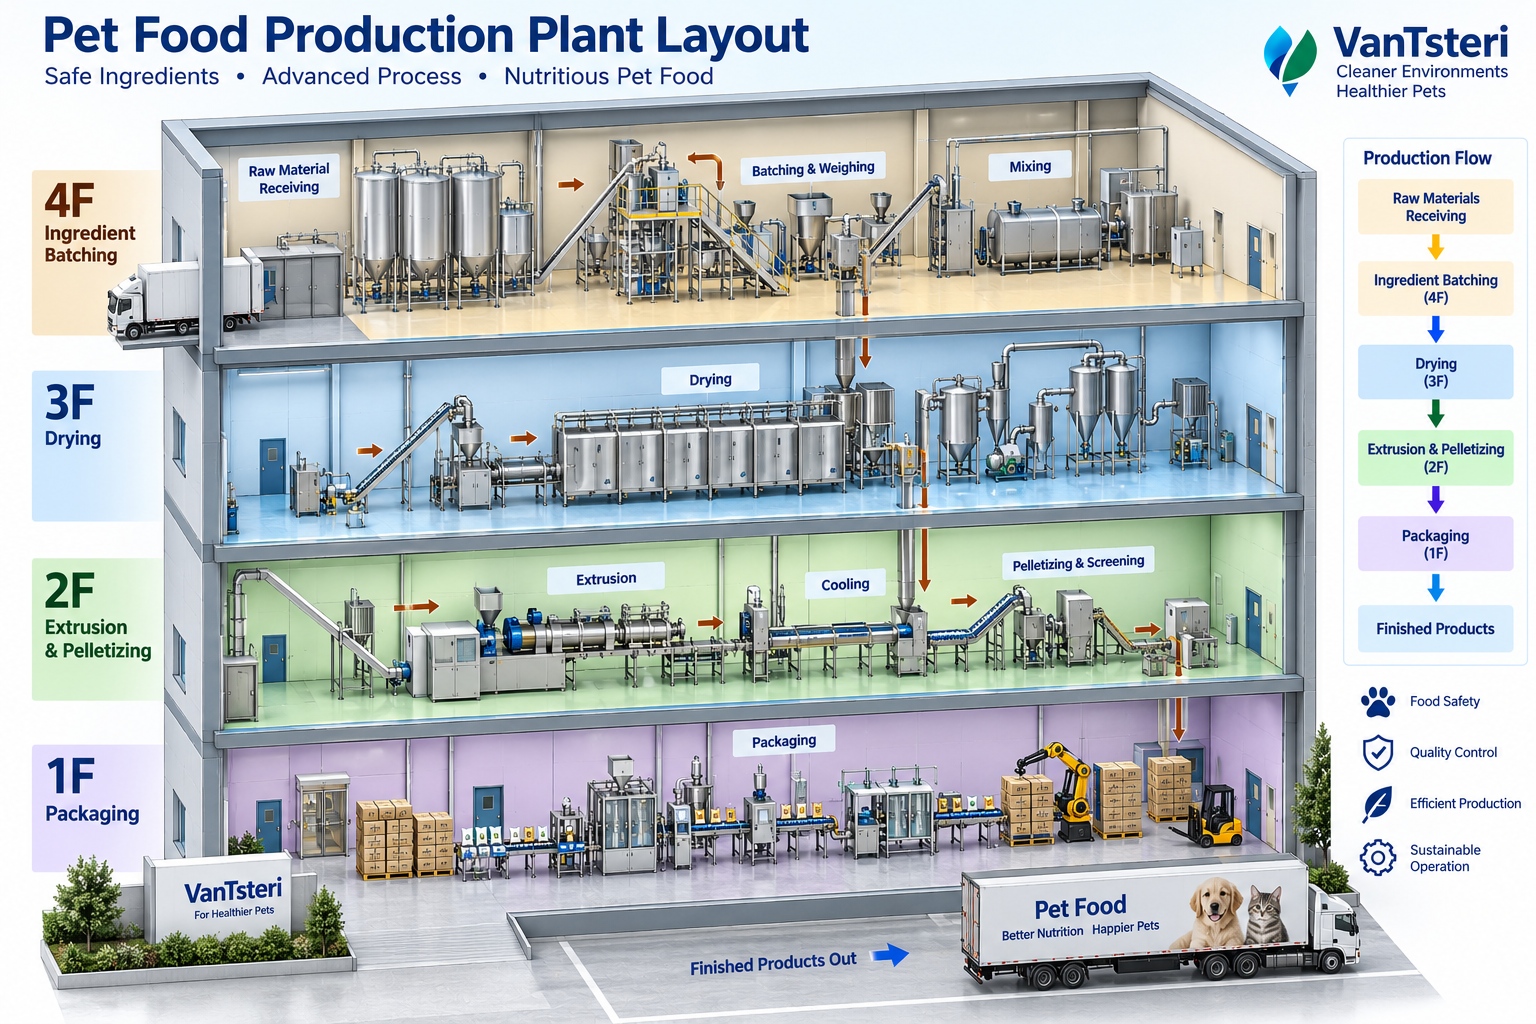
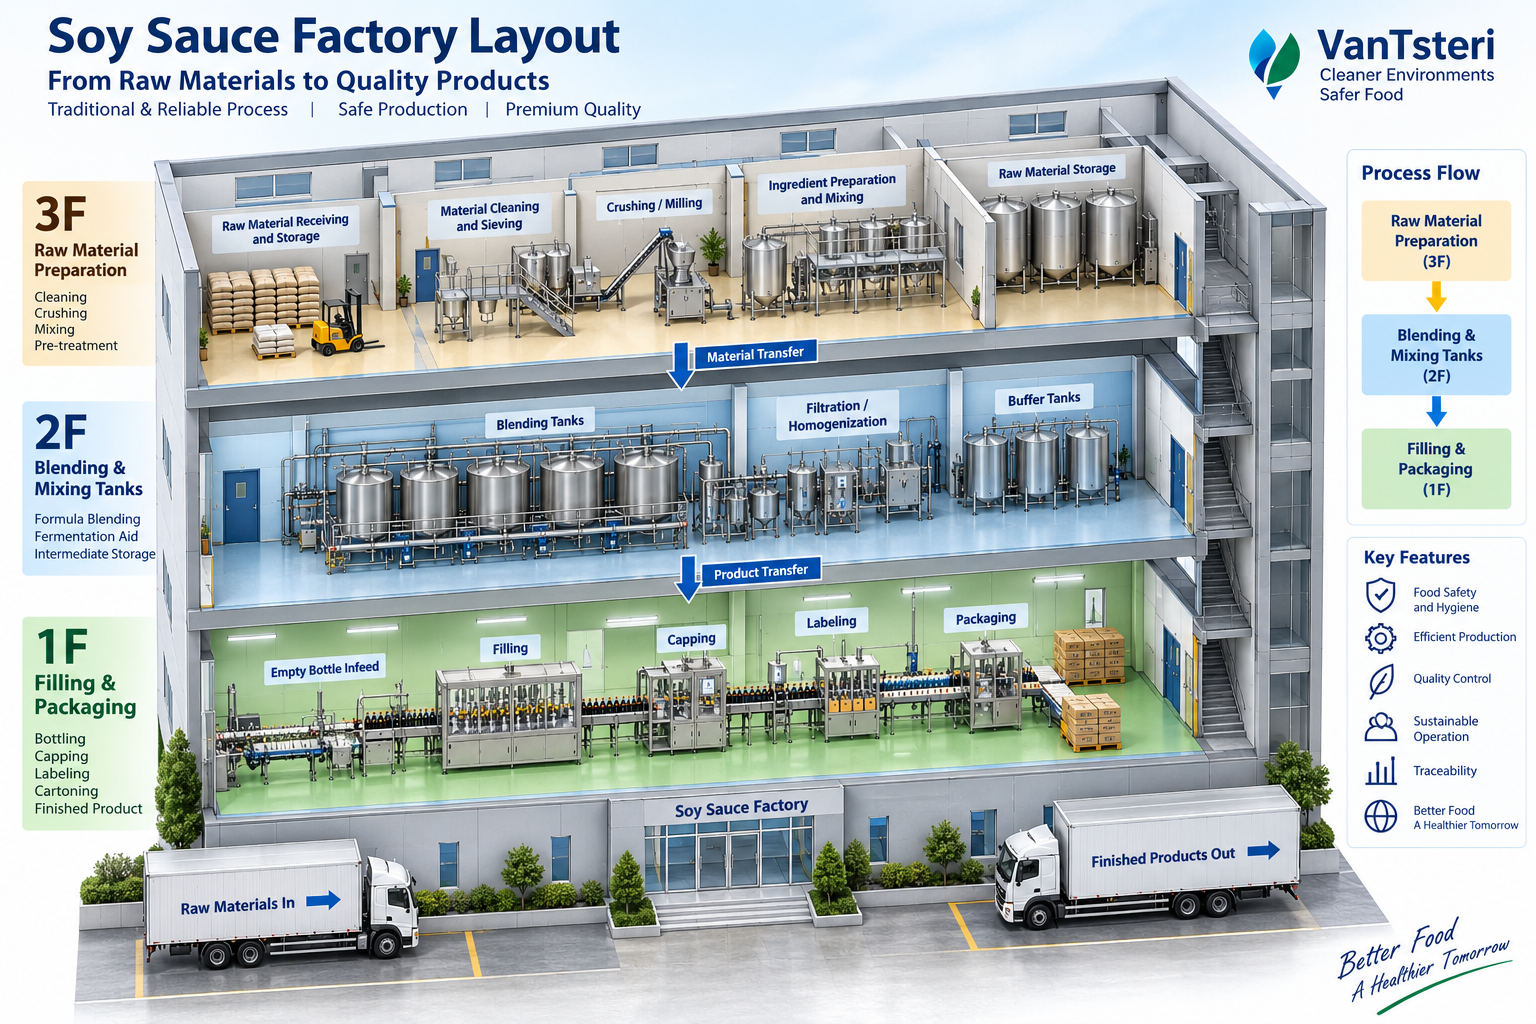
Project process-flow illustration, consistent with the layout confirmed by VanTsteri’s project representative. View original illustration
Project at a glance
Actual treatment area
50,000 m²
On-site work
7 days
Production scope
4 lines
Post-treatment testing
Within one month
Salmonella was not detected in the environmental and product samples tested by the customer during this period.
Tracing findings across the production environment
The project investigation detected Salmonella in environmental samples, pipelines, products and the heating, ventilation and air-conditioning (HVAC) system. These findings guided the treatment priorities across the production process; they do not establish that the organisms detected shared the same strain or source.
The response extended beyond an individual room or piece of equipment. The team used the production flow to identify the areas, systems and locations that needed attention.
VanTsteri organized seven days of integrated on-site treatment, covering production equipment, material-transfer pipelines, the production environment and HVAC-related areas. This was the period of on-site work, rather than a single treatment cycle or continuous application of disinfectant.
The work focused on locations that were easy to overlook or difficult to clean, alongside raw-material management and equipment hygiene measures.
Project highlight: managing complexity across four lines
This project involved a large treatment scope and multiple stages of production. VanTsteri combined investigation findings with on-site organization to coordinate work across four production lines and associated systems, helping reduce the risk of overlooking parts of the production environment.
Evaluating the outcome through the customer’s testing
Within one month after treatment, the customer tested environmental and product samples. Salmonella was not detected in either sample category. These results apply to the actual samples tested and the period covered by this project; they do not represent daily testing, testing of every production batch or independent certification.
The value VanTsteri provided
The project connected contamination findings from multiple stages of production with coordinated treatment across the areas associated with four production lines, followed by the customer’s testing to evaluate the outcome. It illustrates VanTsteri’s ability to organize and carry out work in a large, complex production environment.
If your pet food manufacturing facility is experiencing Salmonella contamination, discuss contamination investigation, treatment of production systems and the environment, and follow-up assessment with VanTsteri.
For suitable pet food production environments, VanTsteri also provides vaporized hydrogen peroxide (VHP) equipment and environmental decontamination services. Suitability and treatment scope are assessed for each site. These related options do not add a specific equipment model or treatment method to the project account above.
This anonymized case is based on VanTsteri’s project materials and information confirmed by its project representative. Customer and supplier identities are withheld.
Investigating internal contamination and treating hard-to-reach process piping.
Looking beyond recurring endpoint results
A pharmaceutical company experienced recurring elevated total viable counts in samples taken at process-pipeline endpoints and engaged VanTsteri to investigate and address the problem. The investigation looked beyond endpoint water samples to attached contamination inside the piping that could continue to affect those results.
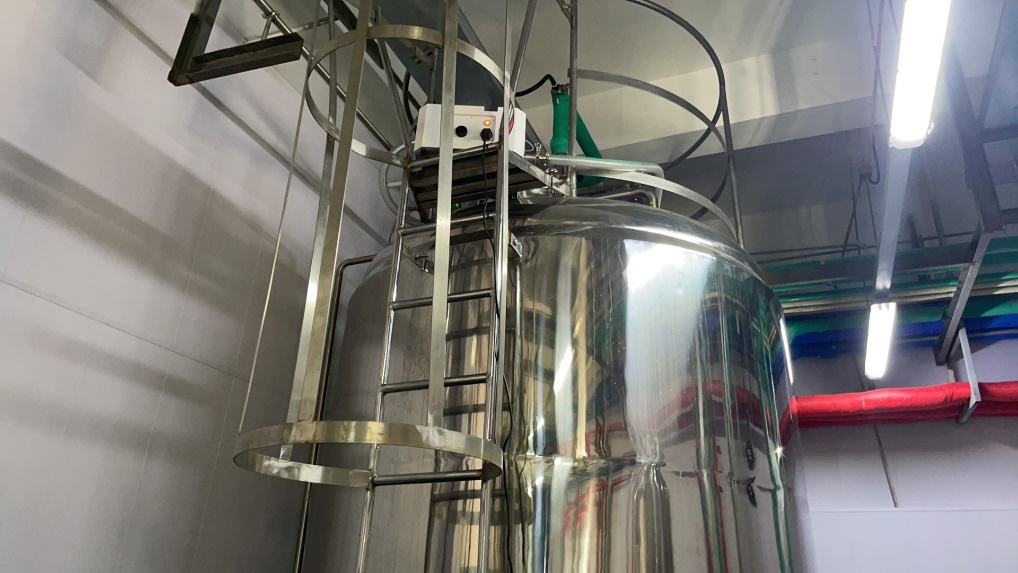
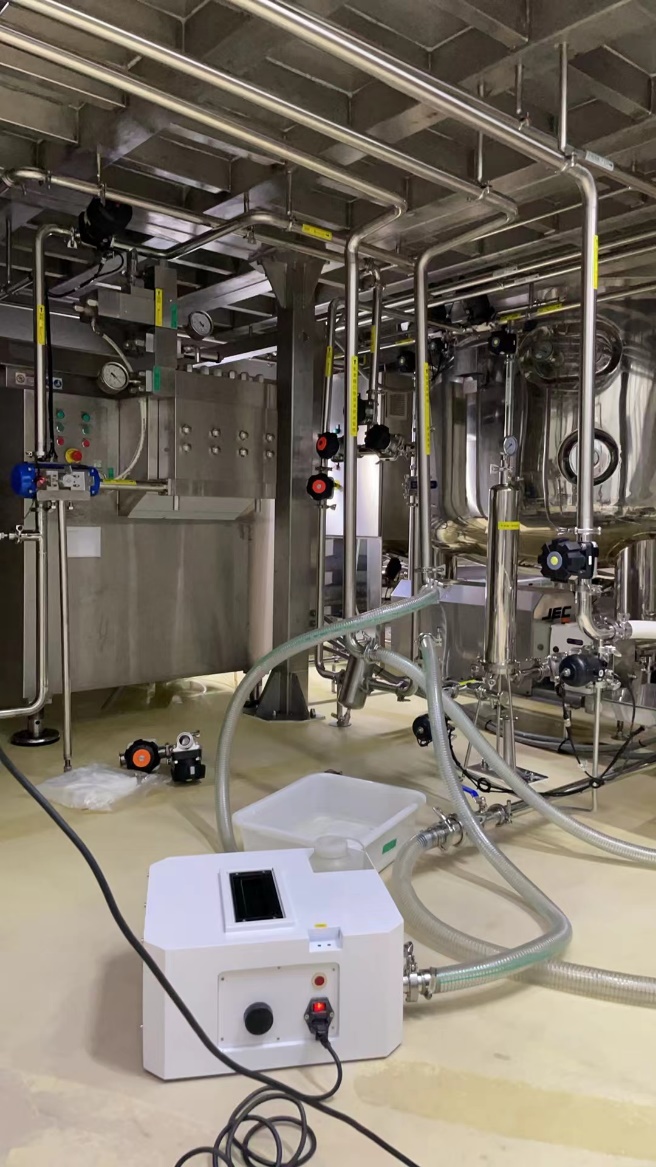
Pharmaceutical equipment and pipeline treatment at this project site. View original photo
The challenge of closed process piping
Internal walls and connection points in closed process piping are difficult to access directly. Treatment needed to consider both the location of contamination and compatibility with the system’s materials. The choice, quantity and conditions of use of liquid treatment chemicals were assessed in relation to those materials.
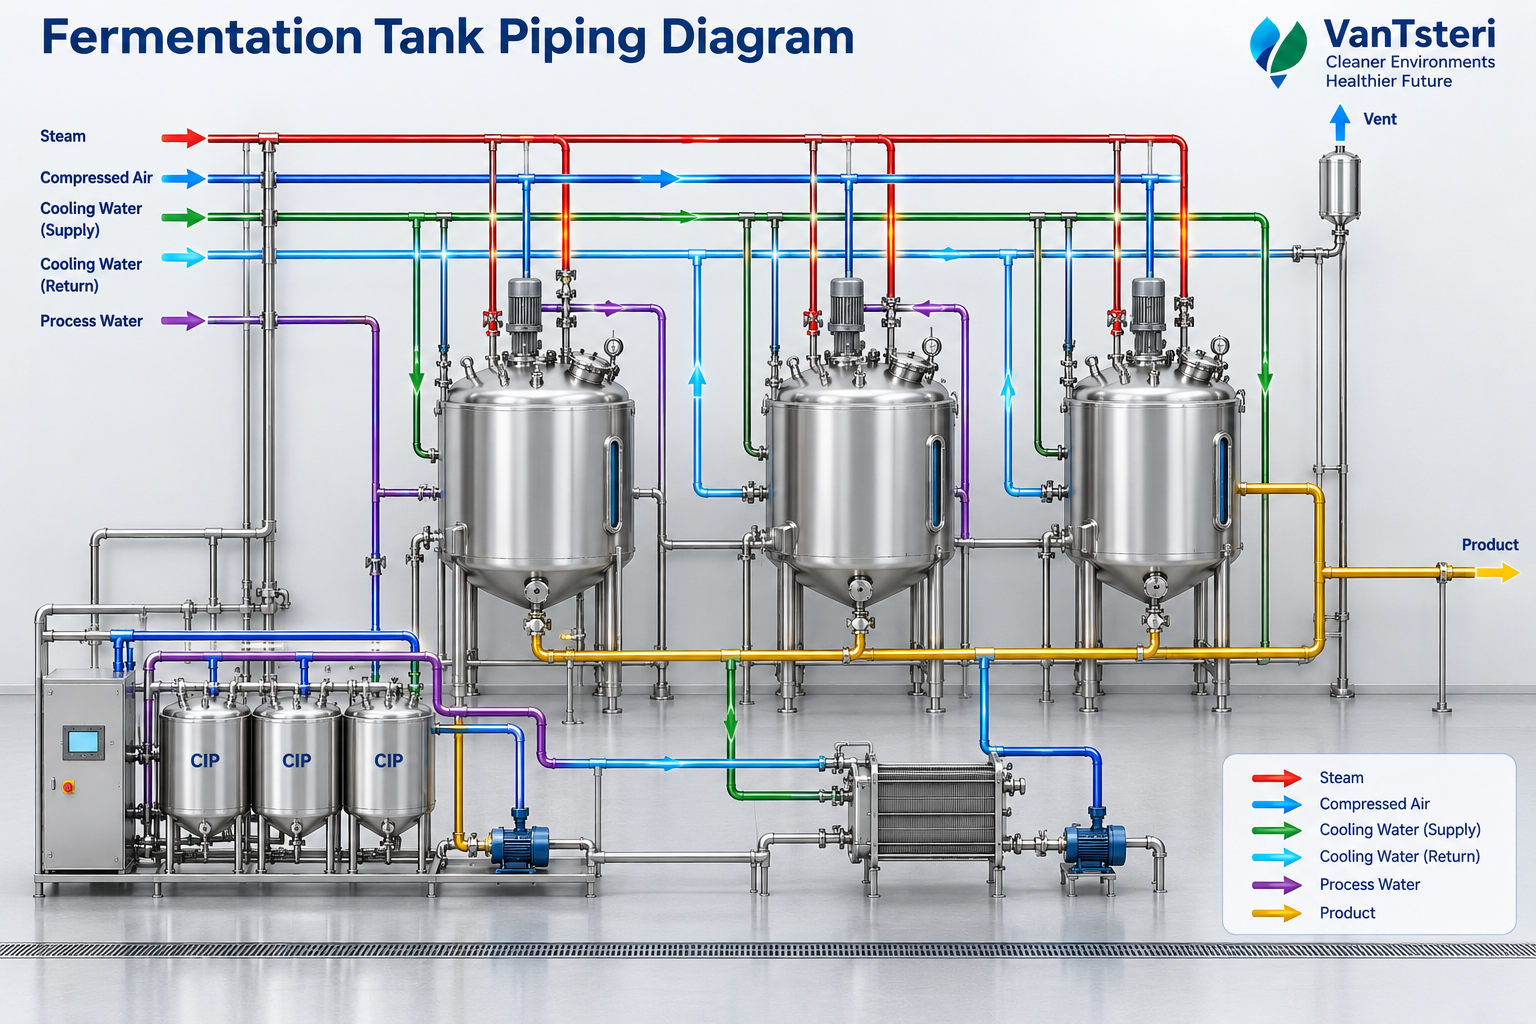
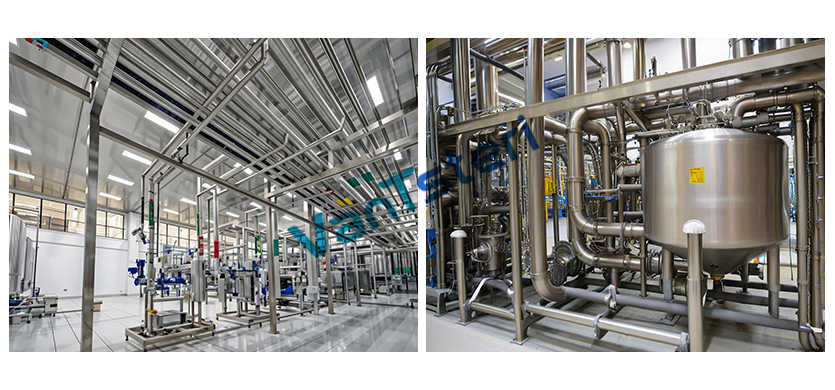
Technical illustration of fermentation tank piping and service connections; not a verified drawing of this project’s configuration. View original illustration
Combining inspection and sampling
The team combined sampling and testing, internal endoscopic inspection, and microscopic examination of samples from connection gaskets and valves to assess biofilm and define the treatment priorities.
VanTsteri applied its own technology to address microorganisms and attached biofilm inside the piping, considering the treatment target, chemical use and material compatibility together.
According to VanTsteri’s project representative, the approach used relatively small quantities of treatment chemicals and specifically targeted attached biofilm. The formulation and proprietary process are not disclosed.
Evaluating the changes through inspection and testing
Following treatment, microbiological testing of both internal-wall samples and water samples showed improvement. Inspection and testing were used together to assess the changes observed in this project.
The value VanTsteri provided
The project connected investigation inside the system with targeted biofilm treatment and post-treatment testing. This helped the customer understand the contamination locations, the direction of the treatment approach and the changes observed after treatment.
If your pharmaceutical equipment or process piping is experiencing recurring microbial abnormalities, discuss contamination investigation, biofilm treatment and outcome assessment with VanTsteri.
VanTsteri also provides vaporized hydrogen peroxide (VHP) equipment and environmental decontamination services for suitable applications. The scope and operating conditions are assessed for each site. This related option is not identified as the biofilm-removal method used in this project.
Coordinated VHP treatment across a large site, with follow-up monitoring.
From product findings to environmental investigation
A food processing facility identified Bacillus contamination in its products and engaged VanTsteri to investigate and address it. Sampling in the associated environment also detected the same microbial species, identified in the original project record as Bacillus cereus. The investigation therefore extended from product testing to contamination assessment across the production environment.
Planning treatment across a large production space
The challenge involved both spore contamination and the size of the production environment. Multiple areas and HVAC-related locations needed to be included in the treatment scope. VanTsteri focused on planning equipment deployment around the site conditions and the areas requiring treatment.
Project layout illustration, consistent with the site arrangement confirmed by VanTsteri’s project representative. View full-size illustration
Coordinating multiple VHP units
The team used its own portable vaporized hydrogen peroxide (VHP) equipment to treat production areas and HVAC-related locations. The project record describes deployment of 15 units, a four-hour treatment period, and a subsequent two-hour HVAC circulation period before testing.
Coordinated deployment was a defining feature of this project: equipment was organized around the site’s space and treatment scope. Completion of a single unit’s operating cycle alone was not used to judge the treatment outcome across the production environment.
Both parties collected samples for testing after treatment. During seven consecutive days of subsequent monitoring, settle-plate, airborne microbial and surface microbial sampling did not detect the target Bacillus previously under investigation. These findings relate to this project’s sampling scope and monitoring period.
According to VanTsteri’s project representative, the customer was satisfied with the treatment outcome.
The value VanTsteri provided
VanTsteri’s service connected the initial product contamination findings with an environmental investigation to define the treatment scope, coordinated deployment of multiple VHP units, and follow-up monitoring to evaluate the outcome. For food facilities with large spaces and multiple production areas, connecting investigation, equipment deployment and testing helps customers understand both the basis for treatment and its results.
If your food facility is facing spore contamination, discuss contamination investigation, VHP equipment deployment and environmental monitoring with VanTsteri.
Case information: This anonymized case is based on VanTsteri’s project record and supplementary information from its project representative. The customer’s identity is withheld.
From environmental findings to coordinated treatment of the laboratory and HVAC systems.
A specific contamination target
A molecular biology laboratory identified environmental nucleic acid contamination and engaged VanTsteri to address it. The project needed to address nucleic acid contamination itself, beyond microbial inactivation alone. Both the treatment plan and the evaluation of its outcome therefore focused on nucleic acid decontamination.
Following contamination findings beyond the workbench
The investigation identified signs of nucleic acid contamination in air, on workbenches and near HEPA-filter outlets. These findings extended the treatment focus from working surfaces to the laboratory environment and its associated heating, ventilation and air-conditioning (HVAC) systems.
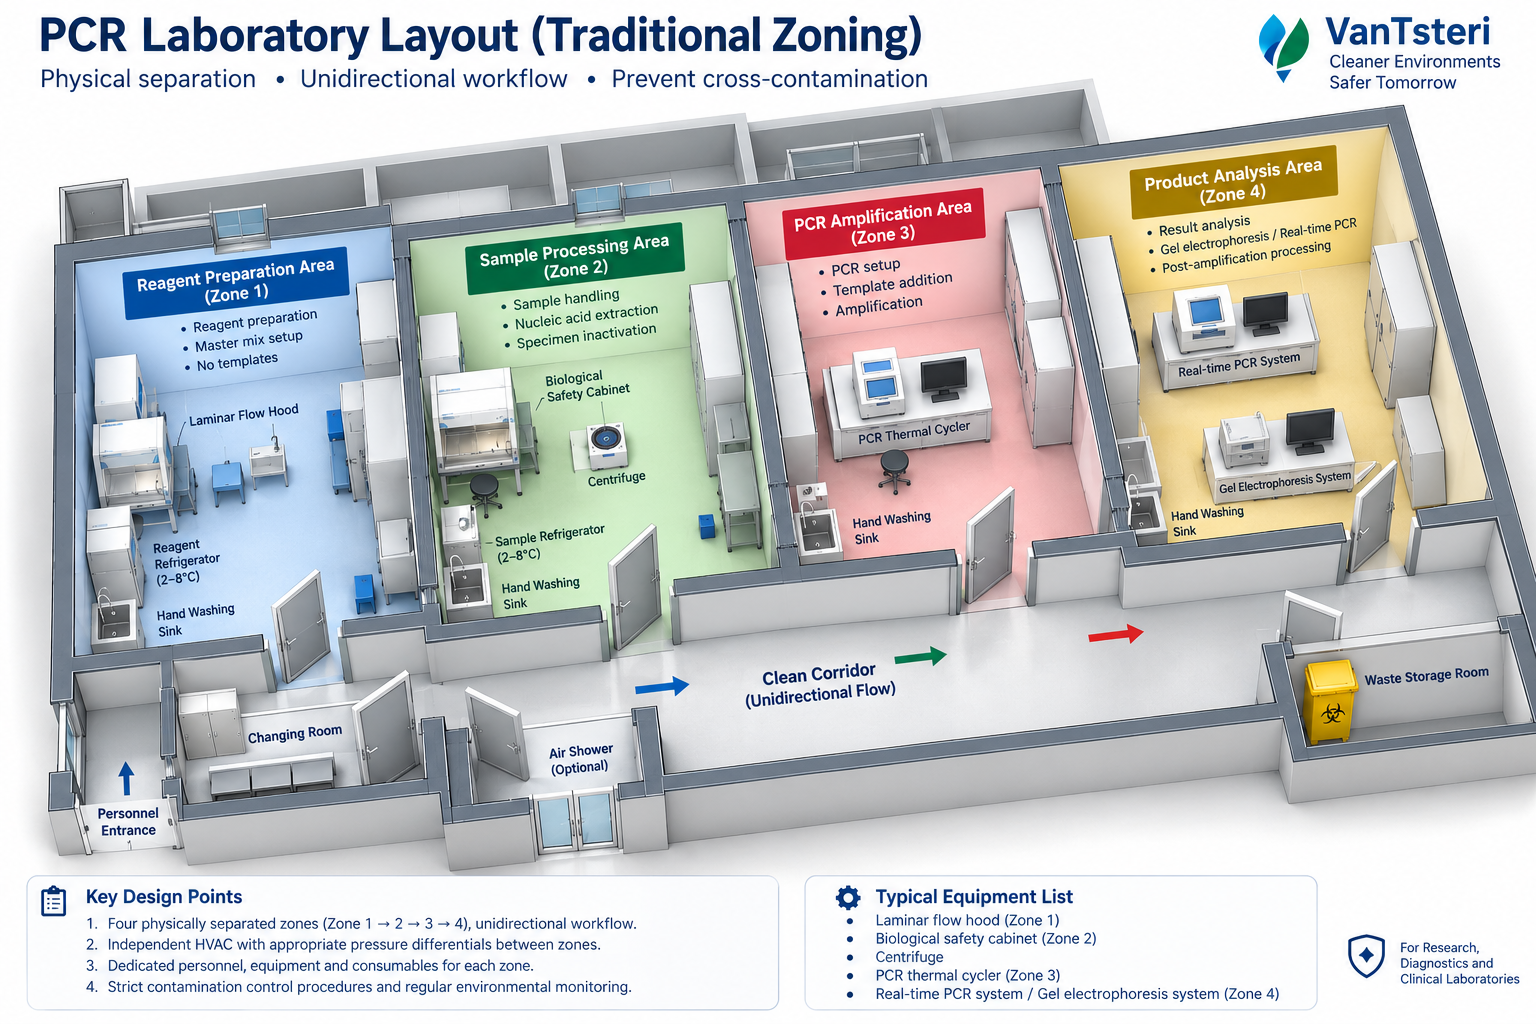
Project layout illustration, consistent with the site arrangement confirmed by VanTsteri’s project representative. View full-size illustration
Treating the laboratory and HVAC systems together
To address these findings, VanTsteri combined its own vaporized hydrogen peroxide (VHP) equipment with dedicated HVAC decontamination equipment in a coordinated treatment plan. The project covered a 300 m² laboratory and three HVAC systems, with a treatment period of five hours.
VanTsteri’s decontamination technology can be used to address nucleic acid contamination. According to a VanTsteri representative, the technology’s nucleic-acid decontamination capability has undergone third-party verification, supporting its application. This case further illustrates its use in treating nucleic acid contamination in a laboratory and its HVAC systems.
Evaluating the outcome through nucleic acid testing
According to the project record, all 120 environmental samples collected after treatment tested negative for the nucleic acid contamination under investigation. These findings relate to the samples tested in this project.
The value VanTsteri provided
The value of this case lies in connecting environmental findings, laboratory and HVAC treatment, and post-treatment nucleic acid testing around a specific contamination problem. This gave the customer a defined treatment scope and relevant test results for evaluating the outcome.
If your PCR laboratory is facing nucleic acid contamination, discuss contamination investigation, laboratory and HVAC decontamination, and post-treatment testing with VanTsteri.
Field images from the VanTsteri company presentation.
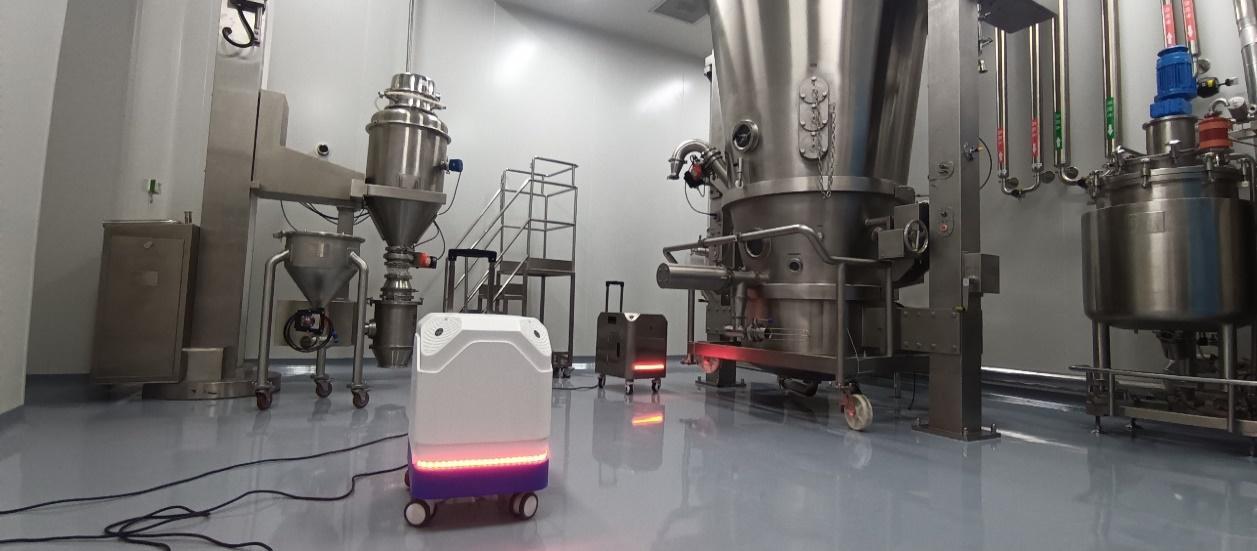
The company presentation shows disinfection equipment deployed in pharmaceutical production areas. Project-specific background and results can be added when the corresponding content is supplied.
Source: VanTsteri company service presentation, page 18.Additional field image from the same presentation page; the images are not identified as a single project.
Microbial contamination control for cold storage environments.
Connect low-temperature service requirements with contamination investigation, on-site support and related equipment.
Cold storageIndustry
Low-temperature environmentsApplication context
Global on-site servicesService availability by project
Understand the contamination concern
Share the affected areas, the history of the concern and any available findings to discuss whether contamination investigation is required.
Describe the operating conditions
The storage temperature, facility layout, equipment and access arrangements help define the project’s service requirements.
Coordinate on-site support
Provide the project country, city and preferred service window so VanTsteri can discuss the on-site scope and scheduling.
Project outcomes
Results achieved.
Operating temperature down to −18°C
KINO SUBZERO is positioned for air-conditioning system and pipeline disinfection, with a low-temperature operating capability down to −18°C as specified by VanTsteri.
Discuss its suitability for the intended system and project conditions with the team.
Disinfection support for biological laboratory environments.
Understand the service scope and connect your laboratory’s contamination concerns with investigation and on-site support.
Biological laboratoriesIndustry
Rooms & equipmentApplication context
Application referenceContent type
The supplied VanTsteri laboratory materials describe disinfection services adapted to different laboratory environments. This page introduces the service scope. Project details will be added as the case content is completed.
When discussing a requirement, distinguish routine environmental disinfection from a response to a recurring contamination concern. The affected rooms, equipment, available findings and operational constraints help define the scope of the discussion.
Understand the reported concern
Review the client’s description of the issue, its history and the available environmental or laboratory findings. Where the source remains unclear, discuss contamination investigation as a related service.
Define the relevant environment
Discuss the rooms and equipment involved, access requirements and the boundaries of the proposed service. The scope should reflect the particular laboratory and its operating requirements.
Agree on project records and review
Before delivery, agree on the information the client needs to document the service and assess its outcome. Project results can be added alongside their supporting records.
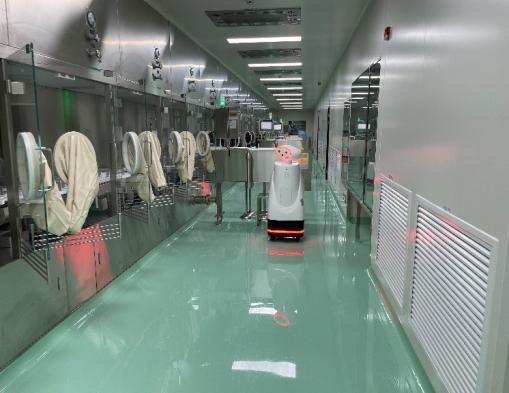
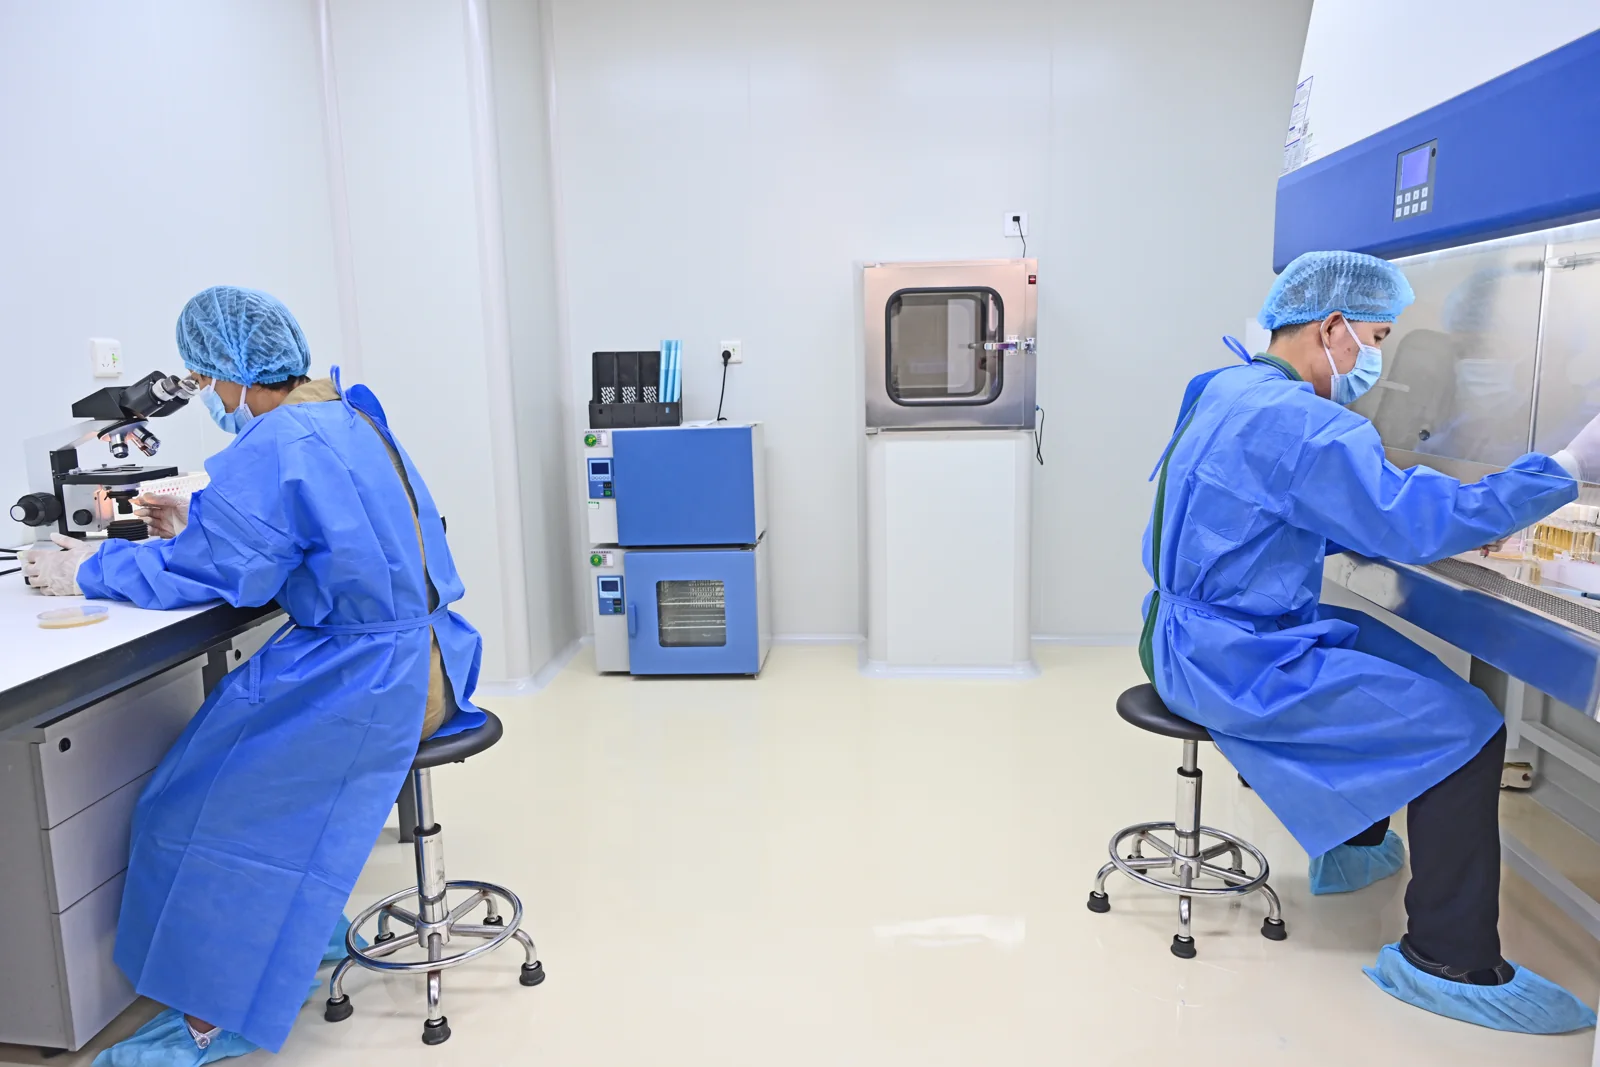
VanTsteri’s own microbiology laboratory, supplied by the company. This is not a customer project photograph.
Explore the laboratory introduction and the contamination investigation service to understand how they relate to your project enquiry.
Prepared from the supplied “Biological laboratory disinfection” website export and the company’s laboratory photographs. Project details and outcome text are awaiting entry.
A pharmaceutical manufacturer identified a suspected contaminating microorganism in its products and engaged VanTsteri to investigate and address the problem. The customer needed to understand where contamination might be located, identify the areas requiring treatment and evaluate the treatment outcome.
Extending the investigation to related environments
VanTsteri extended the investigation to the logistics warehouse and related environments, where testing detected the same microbial species. This finding prompted further investigation of the weighing and sampling rooms, but the same species does not by itself establish the same strain or a common contamination source.
Considering the configuration of the rooms’ HVAC air-purification system and internal areas difficult to reach through routine cleaning, the team suspected contamination within the system. Subsequent testing supported this assessment, giving the treatment a more clearly defined focus.
VanTsteri used KINO SUBZERO vaporized hydrogen peroxide (VHP) decontamination equipment to carry out targeted treatment of the affected HVAC system. The focus was on internal areas that routine cleaning could not readily reach.
KINO SUBZERO is used for HVAC-system and pipeline decontamination, with equipment connections and operating conditions assessed for the site’s system. Hydrogen peroxide can decompose into water and oxygen. Post-treatment testing in this project did not detect residual hydrogen peroxide.
Post-treatment microbiological testing did not detect the microorganism previously under investigation. These findings relate to the samples tested in this project.
The value VanTsteri provided
The project connected contamination investigation, system assessment, targeted VHP decontamination and post-treatment testing. This gave the customer a coordinated approach to investigating contamination, identifying treatment priorities and evaluating the results.
If microbial contamination is affecting your pharmaceutical weighing and sampling rooms, HVAC system or pipelines, discuss a site investigation and VHP decontamination plan with VanTsteri.
This case account and its test findings were provided by VanTsteri’s project representative. The customer’s name and identifying location details are withheld.
A dairy processing facility engaged VanTsteri to investigate and address recurring spore contamination in its dairy products.
This account and the outcomes below are reported by VanTsteri and confirmed by company management. They are not presented as independent third-party verification. The customer is identified only as a dairy processing facility.
Investigation and source tracing
VanTsteri first assessed the microorganism associated with contamination in the dairy products. Considering spore heat resistance and the facility’s routine hot-water flushing process, the team sampled pipeline rinse water and internal pipe surfaces. According to VanTsteri’s project investigation, biofilm was present in the pipeline system.
Pipeline biofilm treatment
VanTsteri reports using its own technology to remove biofilm attached to the internal surfaces of the dairy processing pipelines and associated residues. Treatment effectiveness was evaluated through residue assessment and microbiological testing.
Post-treatment assessment
Post-treatment assessment included pH, total organic carbon (TOC), conductivity and treatment-related chemical residues. Pipeline hydrogen peroxide residues were checked and evaluated against the limit adopted for this project. The sampling medium, test method and basis for that limit are not specified in this account.
COMPANY-REPORTED PROJECT OUTCOMES
Project outcomes
The following figures were provided by VanTsteri’s company representative for this project.
24 hours from decontamination to production resumption
VanTsteri reports that, in this project, 24 hours elapsed from the start of decontamination to the resumption of production. This interval does not describe the entire investigation and cleaning workflow or establish a turnaround time for other projects.
Reported total viable count: <10 CFU/mL
VanTsteri reports a total viable count of <10 CFU/mL in post-treatment surface-sampling liquid collected after sampling tank openings and internal tank walls.
The value refers to the surface-sampling liquid, not the dairy product or a direct surface count in CFU/cm2. It is not a spore-specific log-reduction result or a general statutory food-safety threshold.
Investigation, targeted treatment and verification
According to VanTsteri, investigation, biofilm treatment and post-treatment testing helped the customer locate and address the contamination source in the production pipelines and provided a basis for subsequent contamination control.
Related decontamination options
VanTsteri also provides vaporized hydrogen peroxide (VHP) equipment and environmental decontamination services for suitable applications. The scope and operating conditions are assessed for each site. This related option is not identified as the biofilm-removal method used in this project.
Source: VanTsteri’s company account and the responsible company representative’s clarification. The customer name and identifying location details are withheld. The reported result applies to the described project and sampling context; it does not establish performance for other facilities or operating conditions.
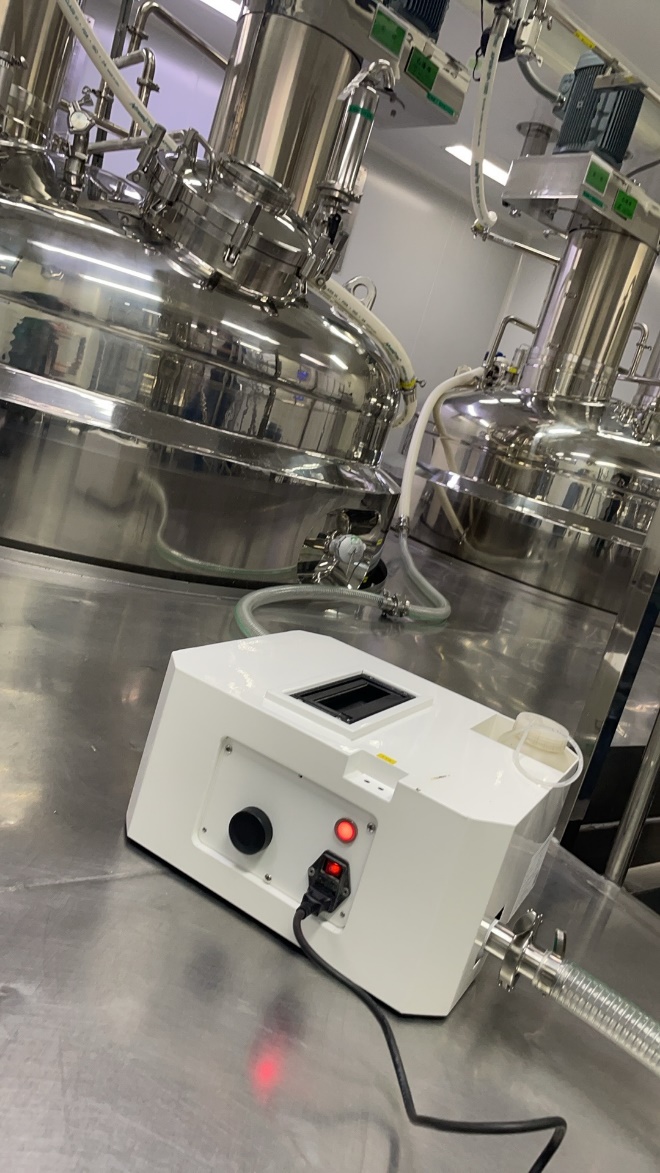
Archive photograph for local review. Project association and publication permission remain subject to separate confirmation.Discuss a contamination project
Optional analytics helps us understand page visits and saved enquiries. Google Analytics loads only if you accept. Rejecting does not affect your enquiry.