Coordinated treatment across four production lines and the production environment.
A large site with complex production systems
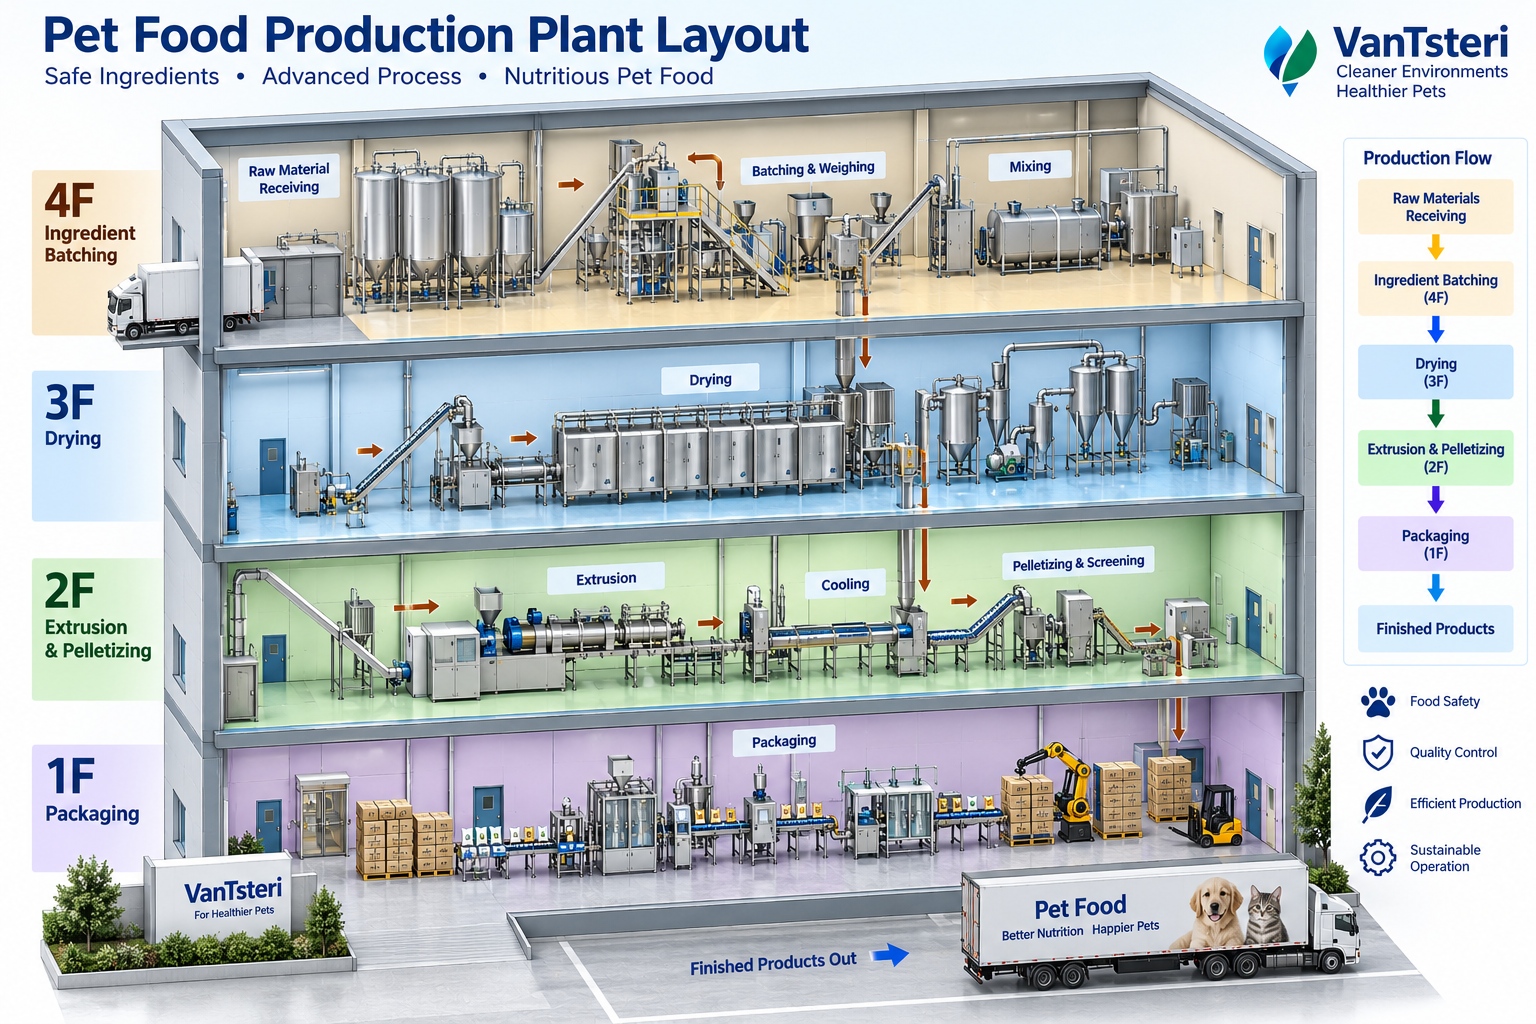
A large pet food manufacturer identified Salmonella contamination and engaged VanTsteri to investigate and address it. The plant operated four production lines, including lines with daily capacities of 10 tonnes or 8 tonnes. The project involved an actual treatment area of 50,000 m², as confirmed by VanTsteri’s project representative. Its scale and the complexity of the production systems created challenges for the on-site work.
Project process-flow illustration, consistent with the layout confirmed by VanTsteri’s project representative. View original illustration
Project at a glance
Actual treatment area
50,000 m²
On-site work
7 days
Production scope
4 lines
Post-treatment testing
Within one month
Salmonella was not detected in the environmental and product samples tested by the customer during this period.
Tracing findings across the production environment
The project investigation detected Salmonella in environmental samples, pipelines, products and the heating, ventilation and air-conditioning (HVAC) system. These findings guided the treatment priorities across the production process; they do not establish that the organisms detected shared the same strain or source.
The response extended beyond an individual room or piece of equipment. The team used the production flow to identify the areas, systems and locations that needed attention.
VanTsteri organized seven days of integrated on-site treatment, covering production equipment, material-transfer pipelines, the production environment and HVAC-related areas. This was the period of on-site work, rather than a single treatment cycle or continuous application of disinfectant.
The work focused on locations that were easy to overlook or difficult to clean, alongside raw-material management and equipment hygiene measures.
Project highlight: managing complexity across four lines
This project involved a large treatment scope and multiple stages of production. VanTsteri combined investigation findings with on-site organization to coordinate work across four production lines and associated systems, helping reduce the risk of overlooking parts of the production environment.
Evaluating the outcome through the customer’s testing
Within one month after treatment, the customer tested environmental and product samples. Salmonella was not detected in either sample category. These results apply to the actual samples tested and the period covered by this project; they do not represent daily testing, testing of every production batch or independent certification.
The value VanTsteri provided
The project connected contamination findings from multiple stages of production with coordinated treatment across the areas associated with four production lines, followed by the customer’s testing to evaluate the outcome. It illustrates VanTsteri’s ability to organize and carry out work in a large, complex production environment.
If your pet food manufacturing facility is experiencing Salmonella contamination, discuss contamination investigation, treatment of production systems and the environment, and follow-up assessment with VanTsteri.
For suitable pet food production environments, VanTsteri also provides vaporized hydrogen peroxide (VHP) equipment and environmental decontamination services. Suitability and treatment scope are assessed for each site. These related options do not add a specific equipment model or treatment method to the project account above.
This anonymized case is based on VanTsteri’s project materials and information confirmed by its project representative. Customer and supplier identities are withheld.